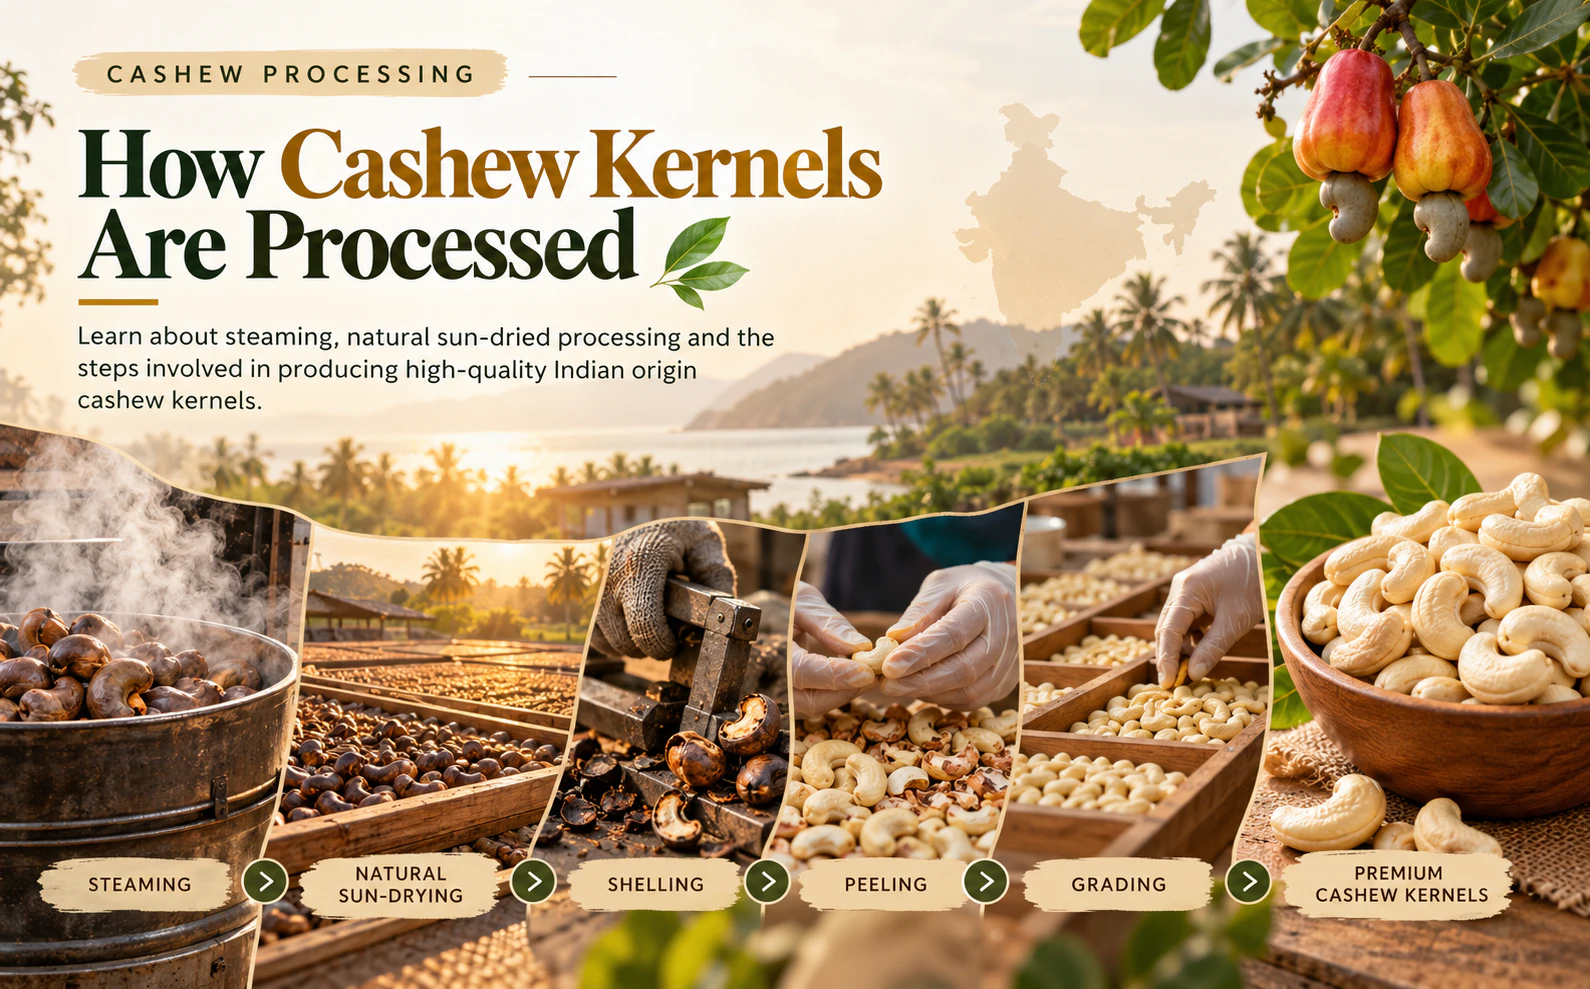
Cashew kernel processing is a carefully controlled series of steps designed to convert raw cashew nuts into clean, safe and high-quality edible kernels. The process begins with the selection of suitable raw cashew nuts and continues through steaming, shelling, drying, peeling, grading and final packing. Each stage plays an important role in maintaining the quality of the kernels.
Indian cashew processing is known for combining traditional handling methods with modern quality control practices. Proper temperature, moisture control and careful handling help preserve the natural colour, texture and flavour of the kernels. Attention to every stage of processing also helps reduce breakage and improve the final appearance of the finished product.
Raw cashew nuts cannot normally be consumed directly because the shell contains cashew nut shell liquid, which requires careful handling during processing. Therefore, the nuts must pass through a controlled processing system before the edible kernel can be safely separated from the outer shell. Proper processing also helps protect the natural quality of the kernel.
The quality of the finished cashew depends on how effectively each processing stage is managed. Excess heat, moisture or rough handling can affect colour, texture and breakage levels. For this reason, experienced processing units focus on maintaining consistent conditions from raw nut reception until the final kernels are graded and packed.
The processing cycle begins with the selection of good quality raw cashew nuts. Nuts are generally checked for size, maturity, moisture level and overall condition before entering the production process. Uniform and mature raw nuts help produce better kernel recovery and more consistent final grades. Damaged or unsuitable nuts may be separated during the initial inspection.
Raw cashew nuts may be sourced from different growing regions depending on availability and production requirements. Proper storage before processing is also important because excess moisture can affect shelling efficiency and kernel quality. The nuts are therefore kept in clean and dry conditions until they are ready for further processing.
Steaming is one of the most important stages in cashew processing. Raw cashew nuts are exposed to controlled steam so that the shell becomes easier to separate from the kernel. The process also helps loosen the internal structure of the nut while maintaining the natural shape of the kernel as much as possible.
Temperature and steaming time must be carefully controlled during this stage. Excessive steaming can affect kernel colour and texture, while insufficient steaming can make shelling more difficult. Skilled processors maintain suitable steaming conditions to achieve a balance between easy shell removal and good kernel recovery.
After steaming, the raw cashew nuts are allowed to cool and rest for a suitable period. This conditioning stage helps stabilize the nuts before they move to shelling. Proper cooling also makes handling safer and can improve the separation between the shell and the inner kernel. The duration may vary depending on the processing system being used.
During conditioning, the nuts are generally stored in a clean and controlled environment. The objective is to allow the heat and moisture introduced during steaming to become balanced. This helps create suitable conditions for shell cutting or mechanical shelling while protecting the kernel inside.
Shelling is the process of removing the hard outer shell from the steamed nut. Depending on the processing unit, this stage may be carried out manually, mechanically or through a combination of both methods. Careful shelling is important because excessive pressure can break the kernel and reduce the percentage of whole cashews obtained.
Skilled handling is especially valuable during this stage because whole kernels generally have higher commercial value than broken pieces. Processing units aim to maximize whole-kernel recovery while maintaining worker safety and efficient production. The separated shells may also be collected for different industrial applications.
After shelling, the kernels still retain a thin outer skin known as the testa. Before this skin can be removed efficiently, the kernels need to be dried. Controlled drying reduces moisture and helps the testa become easier to peel without damaging the kernel underneath.
Drying can be carried out using controlled hot-air systems or other approved processing methods. The objective is not to overheat the kernel but to achieve a suitable moisture level for peeling. Careful drying also contributes to better storage stability and helps maintain consistent product quality.
In some traditional processing systems, natural sun drying is used as part of the preparation or moisture-reduction process. Sun drying relies on controlled exposure to natural sunlight and ventilation to reduce moisture gradually. This method requires proper weather conditions and careful handling to protect the cashews from dust, moisture and environmental contamination.
Natural drying is generally monitored closely because uneven exposure can affect the final quality of the kernels. Cashews may need to be turned periodically to achieve more uniform drying. Clean drying surfaces, proper protection and suitable storage after drying are essential for maintaining hygiene and product consistency.
Once the kernels are properly dried, the thin brown skin surrounding the cashew kernel is removed. This process is known as peeling or testa removal. Peeling may be done manually or with suitable machinery depending on the production scale and the quality specifications required.
The peeling stage requires care because the exposed kernel can break easily if handled roughly. Processors try to remove the skin completely while keeping the kernel intact. After peeling, the kernels are inspected and any remaining skin particles or unsuitable pieces are removed before grading.
Grading is the process of separating cashew kernels according to size, shape, colour and level of breakage. Common grades include whole kernels, splits, pieces and several size-based categories such as W210, W240, W320 and W450. Each grade serves different market and food-industry requirements.
Whole white kernels generally receive greater commercial attention because of their appearance and uniformity. However, broken and split kernels are also widely used in confectionery, bakery products, sweets, sauces and processed food applications. Accurate grading helps buyers choose the appropriate product for their specific usage.
Before packing, cashew kernels go through detailed quality inspection. Kernels may be checked for colour, size, foreign matter, damaged pieces and other visible defects. Sorting helps ensure that each batch matches the quality specifications required for domestic and international markets.
Modern processing facilities may also use metal detection, laboratory testing and food safety procedures to strengthen quality control. These checks help ensure that finished kernels are suitable for packing and distribution. Consistent inspection at different stages also reduces the possibility of unsuitable kernels reaching the final product.
Moisture control is an important part of preparing cashew kernels for storage. Excess moisture may affect texture and shelf stability, while kernels that are too dry can become more brittle and prone to breakage. Therefore, processors aim to maintain a suitable moisture level before packaging.
The kernels may be rested and conditioned after grading so that moisture remains balanced throughout the batch. Proper moisture management helps preserve the natural texture of the cashews during transportation and storage. It also supports better product consistency when cashews reach the customer.
Once the kernels have passed quality inspection, they are prepared for final packaging. Commercial cashews are often vacuum packed or packed using controlled methods that reduce exposure to air and moisture. Suitable food-grade packaging helps protect flavour, texture and freshness during storage and transportation.
Packaging may vary depending on whether the product is intended for wholesale, retail, export or food manufacturing. Bulk cashews are commonly packed in larger food-grade units, while retail products may be packed in smaller consumer-friendly formats. Proper sealing and labeling also support traceability and product handling.
Hygiene is essential throughout every stage of cashew kernel production. Processing areas, machinery, storage spaces and handling equipment should be kept clean to reduce the risk of contamination. Workers may also follow suitable hygiene practices such as clean uniforms, gloves and controlled access to production areas.
Food processing facilities may follow documented cleaning procedures, pest-control systems and quality-management practices. These measures help maintain a consistent production environment and support food safety. Hygiene controls become especially important for cashew kernels intended for international export markets.
Modern cashew processing has become more efficient with the use of improved steaming systems, shelling machines, drying equipment and sorting technology. These systems help processors handle larger quantities while maintaining more consistent processing conditions. Automation can also reduce manual handling in selected stages of production.
Despite technological improvements, skilled inspection and quality control remain important. Cashews are delicate products, and human supervision is often required to monitor colour, breakage and overall appearance. The combination of technology and experienced processing helps produce consistent high-quality kernels.
Indian cashew kernels are widely used in domestic and international markets because of their flavour, texture and established processing tradition. India has a long history of cashew processing, with experienced workers and processing units handling many different commercial grades. This experience contributes to consistent sorting and quality preparation.
Indian origin kernels are used in retail snacks, confectionery, bakery products, sweets, hospitality and food manufacturing. Different grades are available for different market requirements, allowing buyers to choose whole, split or broken kernels depending on their application and budget.
Proper storage is necessary after cashew kernels have been processed and packed. Finished cashews should generally be kept in clean, cool and dry environments away from direct sunlight and excessive humidity. Suitable storage conditions help protect the natural flavour, texture and overall quality of the product.
Storage areas should also be protected from pests, strong odours and environmental contamination. Proper stock rotation and packaging inspection are useful for maintaining consistency over time. For export shipments, careful warehouse handling and transportation practices are also important for protecting the kernels until delivery.
Cashew kernel processing involves several carefully managed stages, beginning with raw nut selection and continuing through steaming, conditioning, shelling, drying, peeling, grading, inspection and packing. Each stage contributes directly to the appearance, texture and overall quality of the finished cashew kernel.
A combination of controlled processing, natural drying methods where suitable, proper hygiene, careful handling and strong quality inspection helps produce high-quality Indian origin cashew kernels. From whole premium grades to splits and pieces, properly processed cashews can meet a wide range of retail, food-service and industrial requirements.